
ROSTRA Tools tool shop: press tools, mould making and CNC machining
Tool shop in Vizovice, Czech Republic: we design and build press tools, make injection moulds for plastics and machine precision parts on CNC machines. Know-how built up since 2000 — our tools stamp parts for Škoda, BMW, Porsche, Volvo, Toyota and other brands.
- max. tool length
- 5 000 mm
- max. tool weight
- 30 t
- employees
- ~40
- automotive supplier · ISO 9001, 14001, 45001
- Class A


From press tool to precision machined part
Press tools
Progressive, tandem and transfer press tools for the automotive industry.
Injection moulds
Moulds for injection-moulded plastic parts — from smaller components to visible and structural parts. References: VW BULB-CAP, VW FTI-HOLDER.
Precision machined parts
Contract CNC machining — milling, wire EDM, die-sinking EDM, grinding.
Special fixtures
Inspection fixtures for measuring stampings and assemblies, assembly and welding fixtures.
Forging dies
For projects that combine stamping with forging.
CNC machining: what we have in our halls
5-axis CNC machining centres 2 machines
Palletising on the HERMLE C32 centre lets the operator prepare a batch of clamped workpieces for a whole week — the machine picks up the next piece by itself and machines it.
| Machine | Model | X | Y | Z |
|---|---|---|---|---|
| HERMLE (with palletising) | C 32 | 650 | 650 | 500 |
| HERMLE | C 42 U | 800 | 800 | 550 |
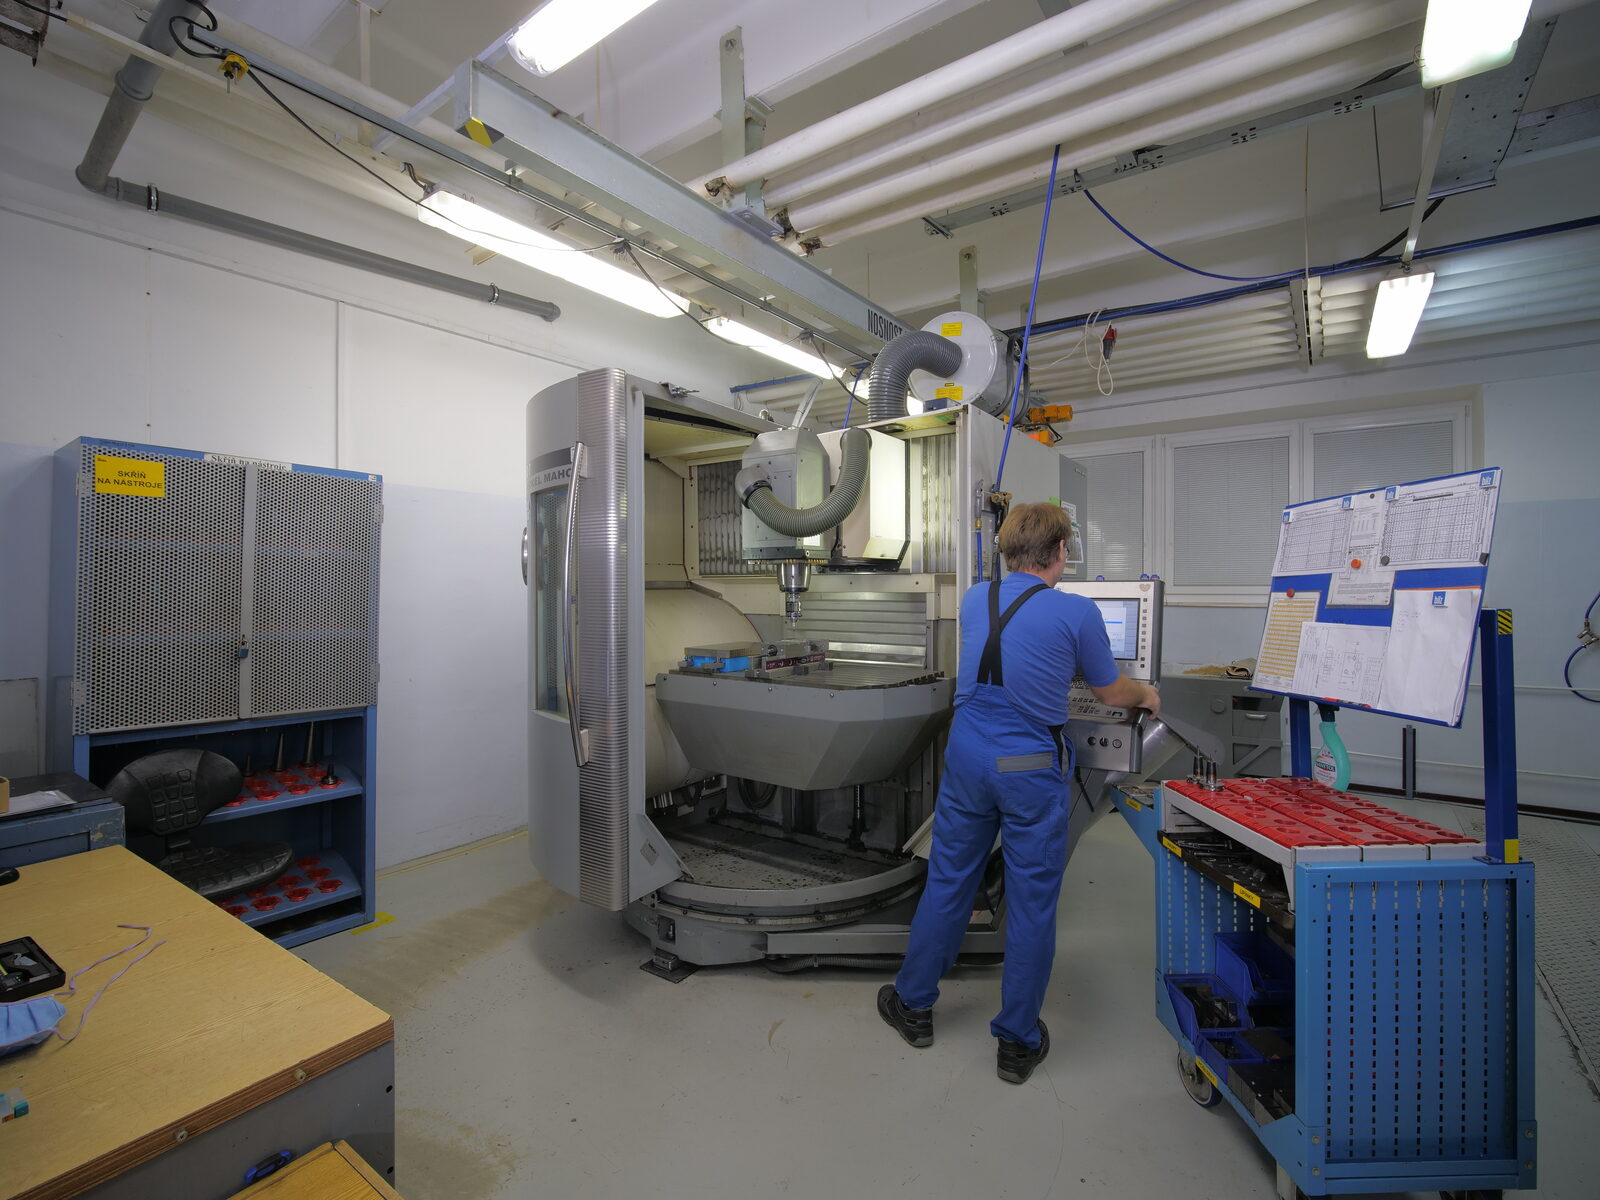
3-axis CNC machining centres 5 machines
| Machine | Model | X | Y | Z |
|---|---|---|---|---|
| DECKEL MAHO | DMC 125P hi-dyn TNC 426 | 1220 | 880 | 800 |
| DECKEL MAHO | DMC 100V hi-dyn TNC 426 | 1000 | 880 | 500 |
| DECKEL MAHO | DMU 60T TNC 530 | 630 | 560 | 560 |
| TAJMAC–ZPS | MCFV 1060 Standard | 1016 | 610 | 760 |
| TAJMAC–ZPS | MCFV 1060 Standard | 1016 | 610 | 760 |
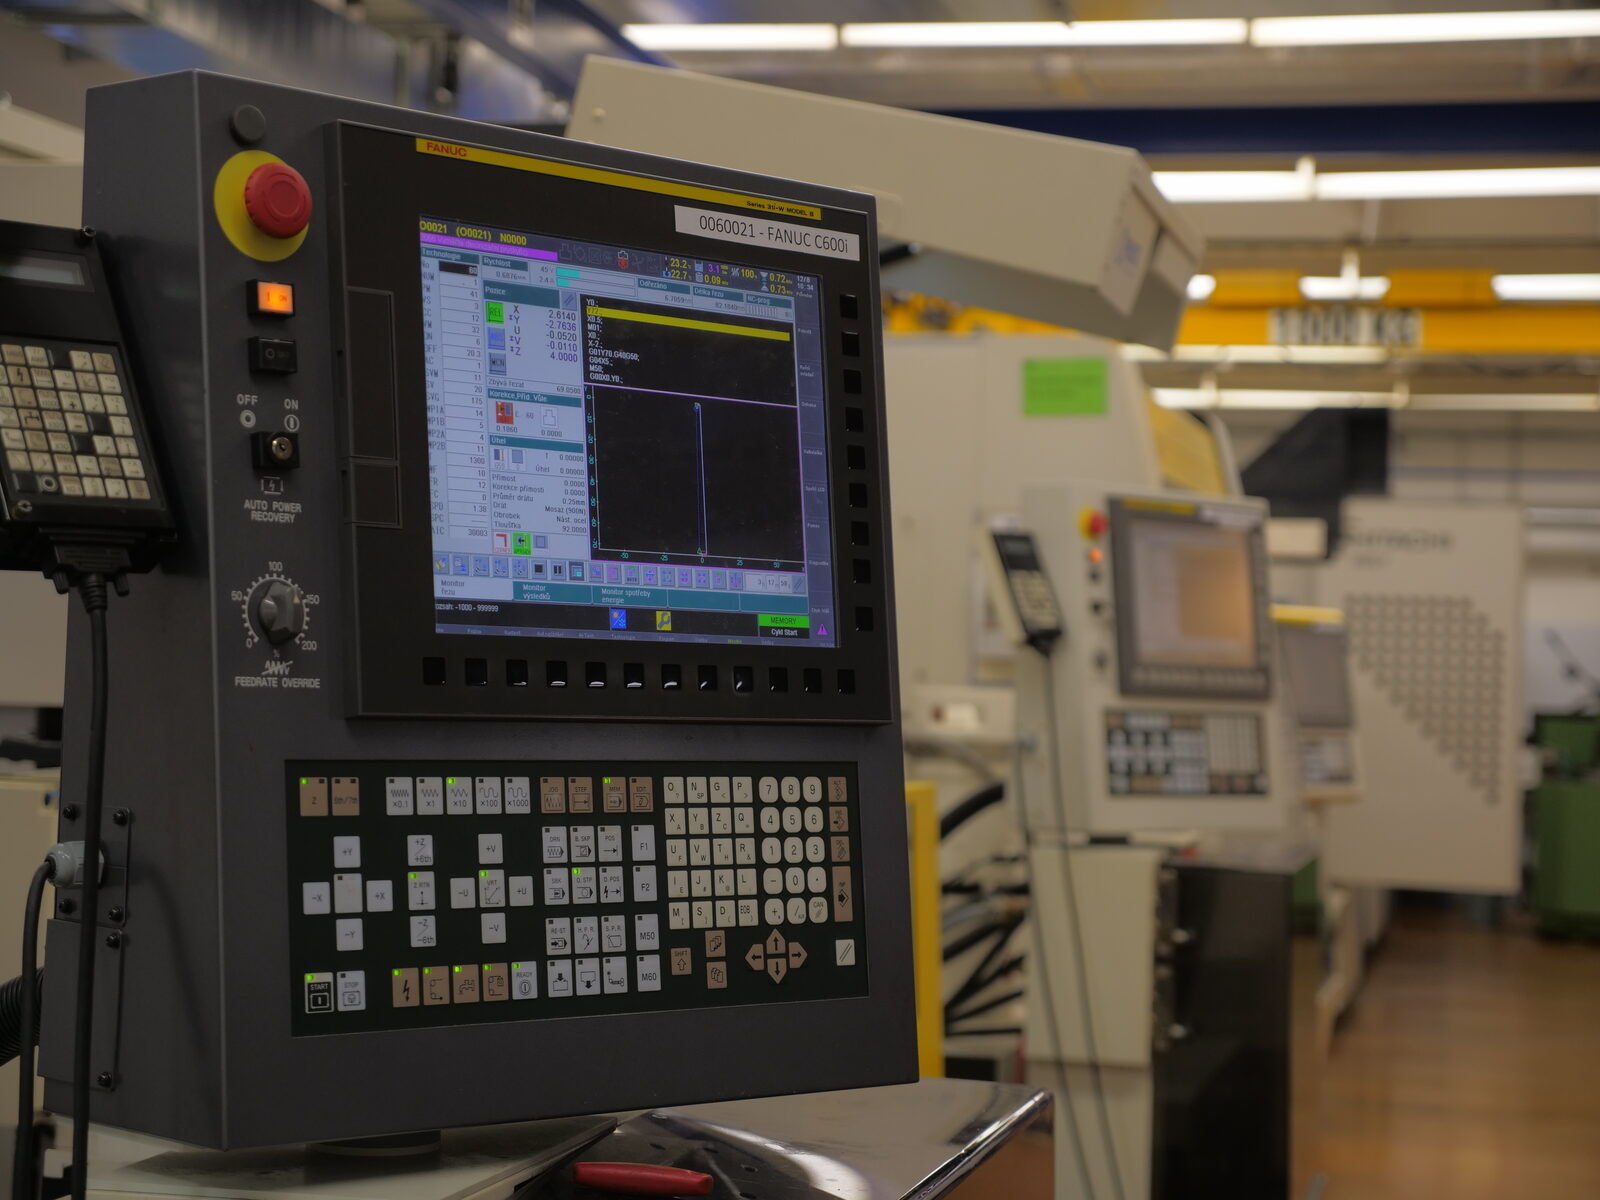
Wire EDM machines 8 machines
Machines with palletising run unattended overnight and at weekends — the automatic loader takes the next workpiece from the magazine as soon as the previous one is finished.
| Machine | Note | X | Y | Z |
|---|---|---|---|---|
| 2× FANUC RC C600iB | with EROWA palletising | 400 | 500 | 440 |
| FANUC α-C600iA | — | 1050 | 820 | 310 |
| FANUC α-C600iA | — | 1050 | 820 | 310 |
| FANUC α-1iD CE | — | 600 | 400 | 310 |
| HITACHI 355Y | — | 500 | 350 | 300 |
| HITACHI 355R | — | 450 | 300 | 300 |
| HITACHI 254Y/FF3 | — | 250 | 400 | 210 |
Die-sinking EDM 1 machine
Our EDM cell machines shapes that cannot be milled — tiny electrical discharges in a dielectric let us machine even very hard materials with a high-quality surface and high precision.
| Machine | Model | X | Y | Z |
|---|---|---|---|---|
| DECKEL | DE 25 C Multiform 4 | 500 | 350 | 350 |
Grinding 6 machines
| Surface grinders | Model | X | Y |
|---|---|---|---|
| ZIERCH GmbH | ZT 612, horizontal surface | 1200 | 700 |
| AQUASTYL SLOVAKIA | BRH AQ500, horizontal surface | 1000 | 500 |
| ZVL | BRH 20.05, horizontal surface | 630 | 230 |
| ZVL | BRH 20.02, horizontal surface | 630 | 230 |
| Cylindrical grinders | Model | Ø | L |
|---|---|---|---|
| TOS | BU 28, universal | 160 | 630 |
| TOS | BU 16, universal | 160 | 320 |
Tool assembly
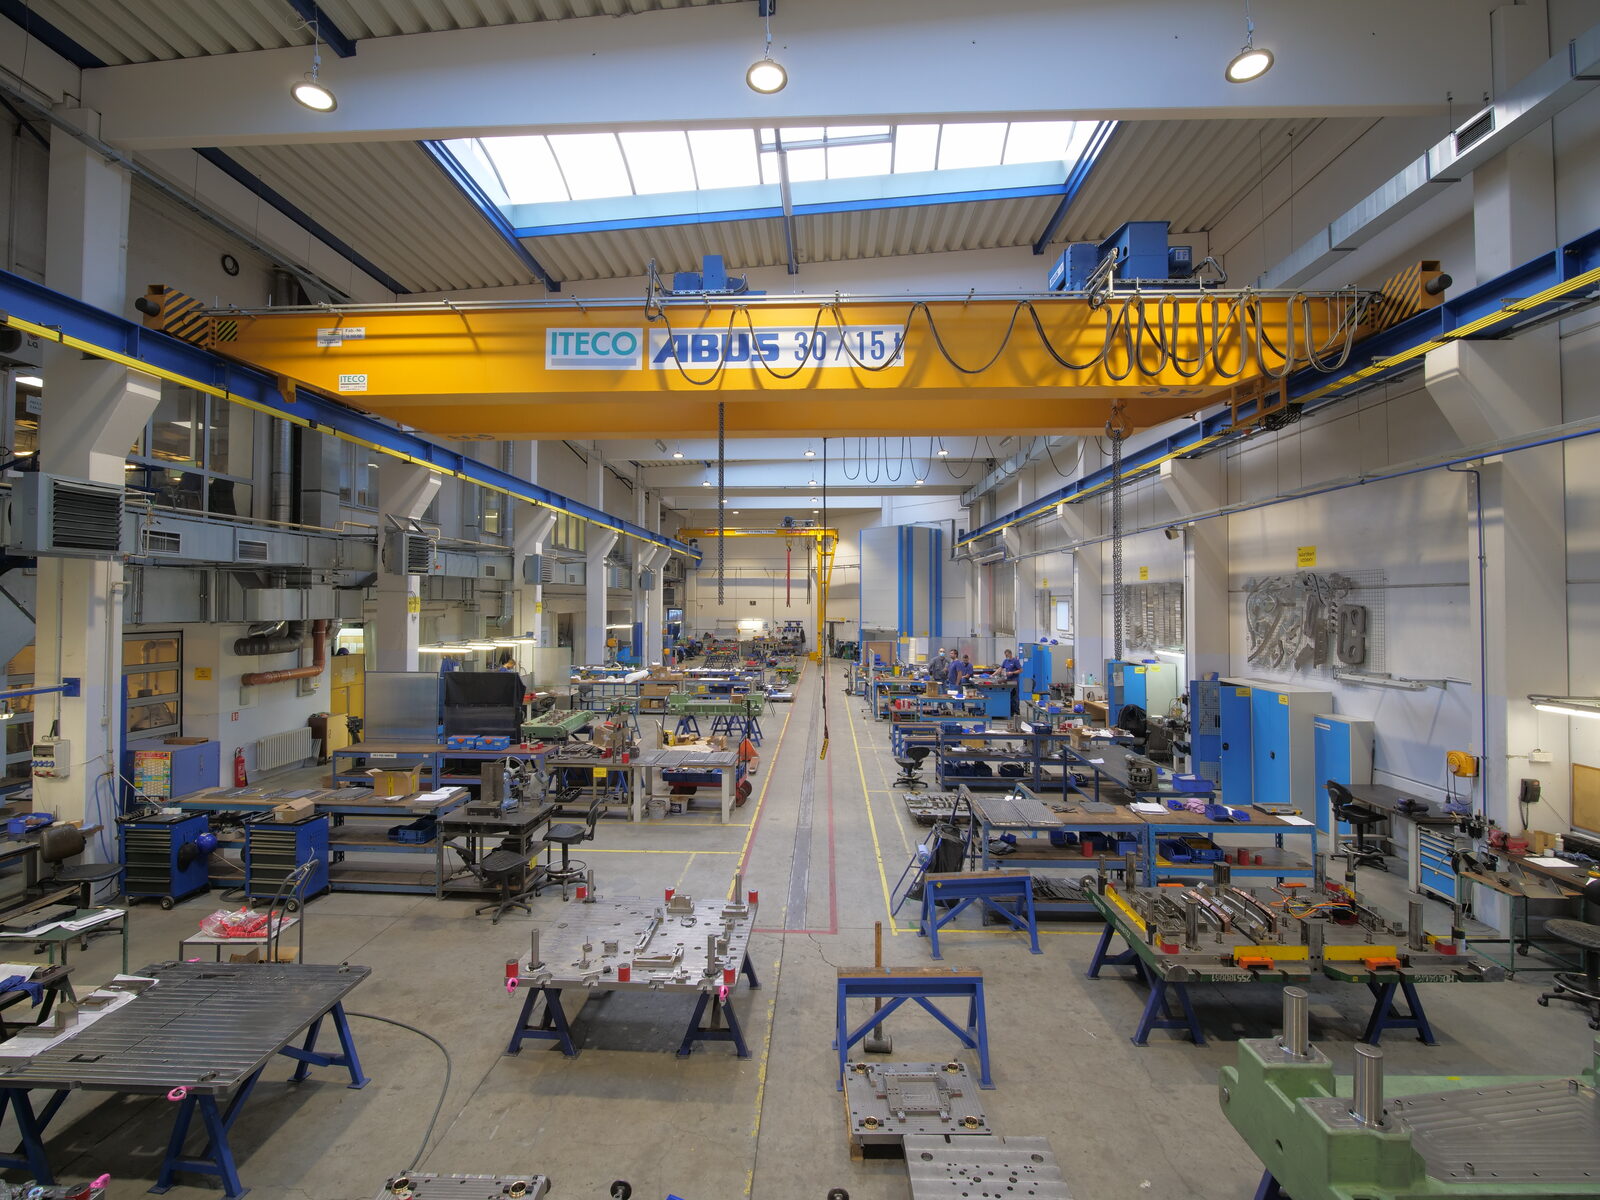
Maximum tool length 5 000 mm, maximum weight 30 t. Tool try-out before release to series production takes place in our sister press shop, ROSTRA Stamping.
Note: ROSTRA Tools does not currently offer turning — the old SAY 48 and SAY 63 automatic lathes were retired several years ago.
Maximum workpiece dimensions on the milling centres and guaranteed tolerances: [Maximum workpiece dimensions and tolerances to be added]
Complete tool development
The design department is a stable team of designers and process engineers. We use Siemens NX as our main CAD/CAM for tool and mould design, SolidWorks with the SolidVision add-on for 3D modelling, and the specialised Visi software for press tools.
Before building a tool we carry out stamping simulations to verify manufacturability — shape, springback, risk of cracks and wrinkling. The simulations are done externally by specialists and the results are fed back into the design.
We are currently moving to drawing-less documentation — operators get colour-coded 3D models directly on the screen at the machine, with no paper drawings. Fewer errors, faster orientation, better traceability.

“The basis is a perfectly chosen stamping technology backed by verified simulation. The result is a stable tool with a long service life.”
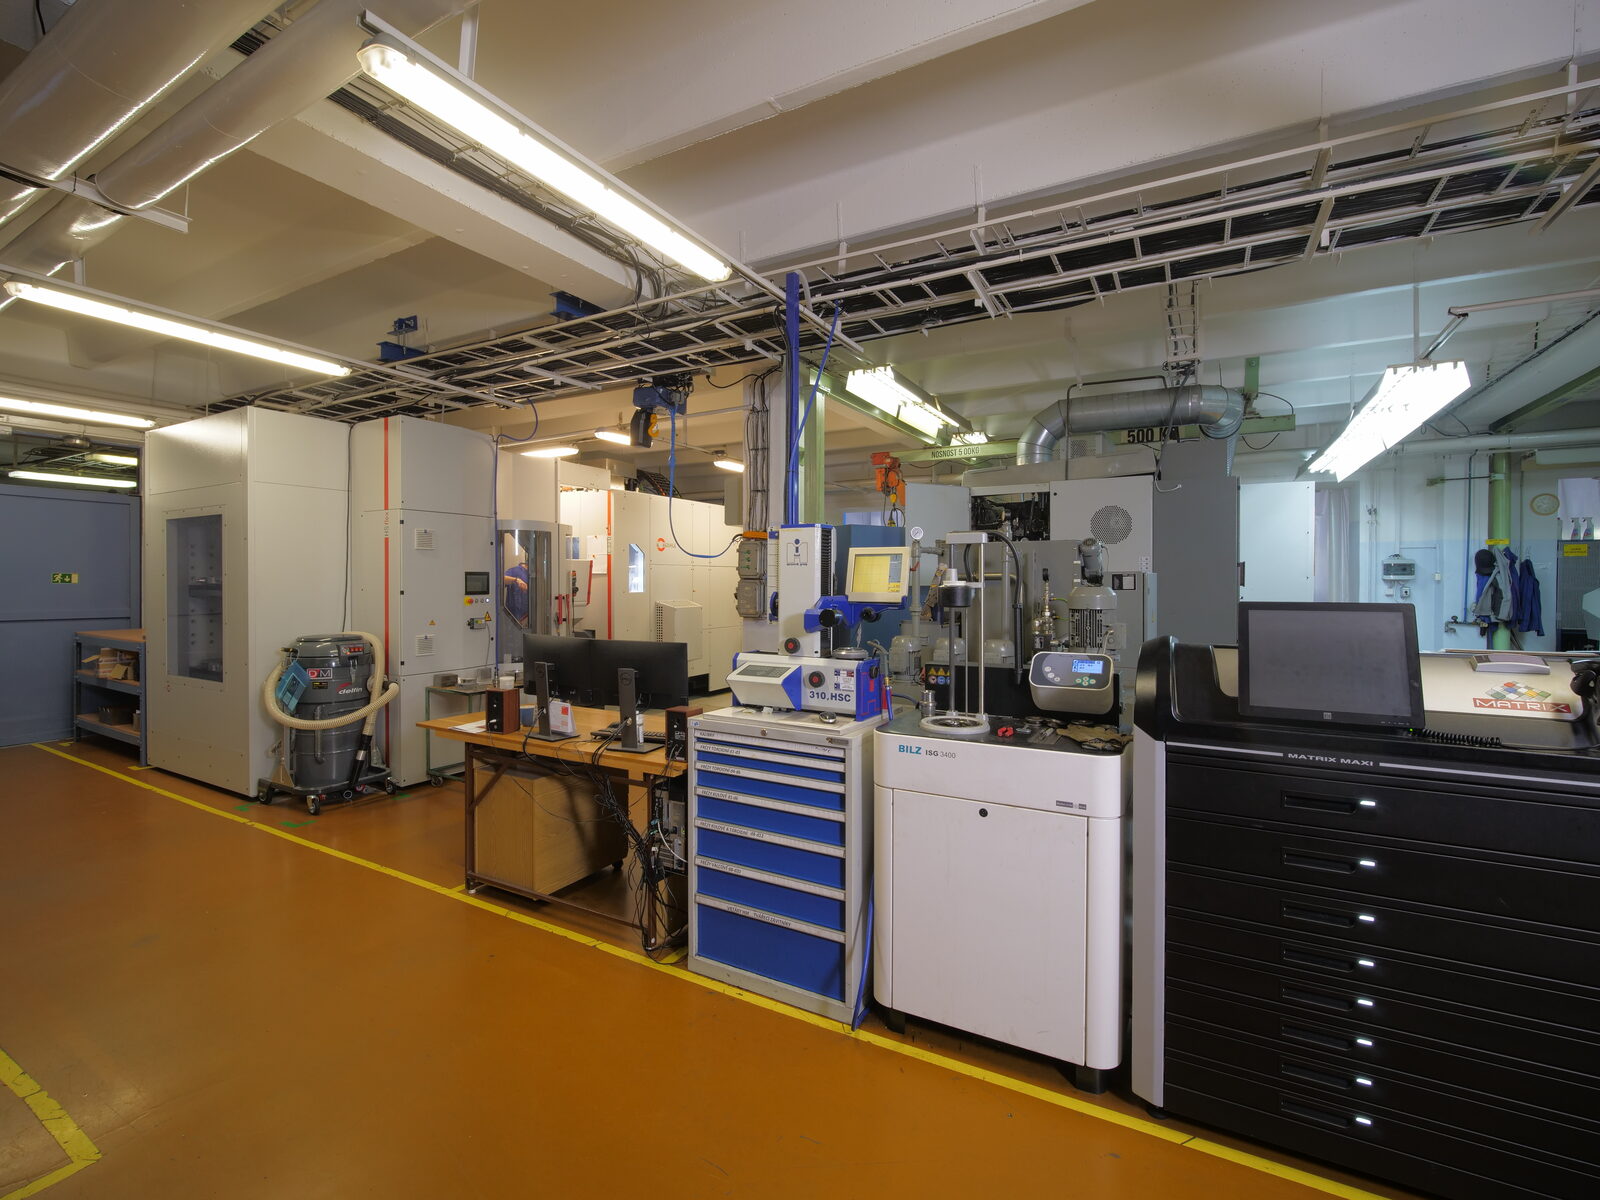
Measurement and inspection
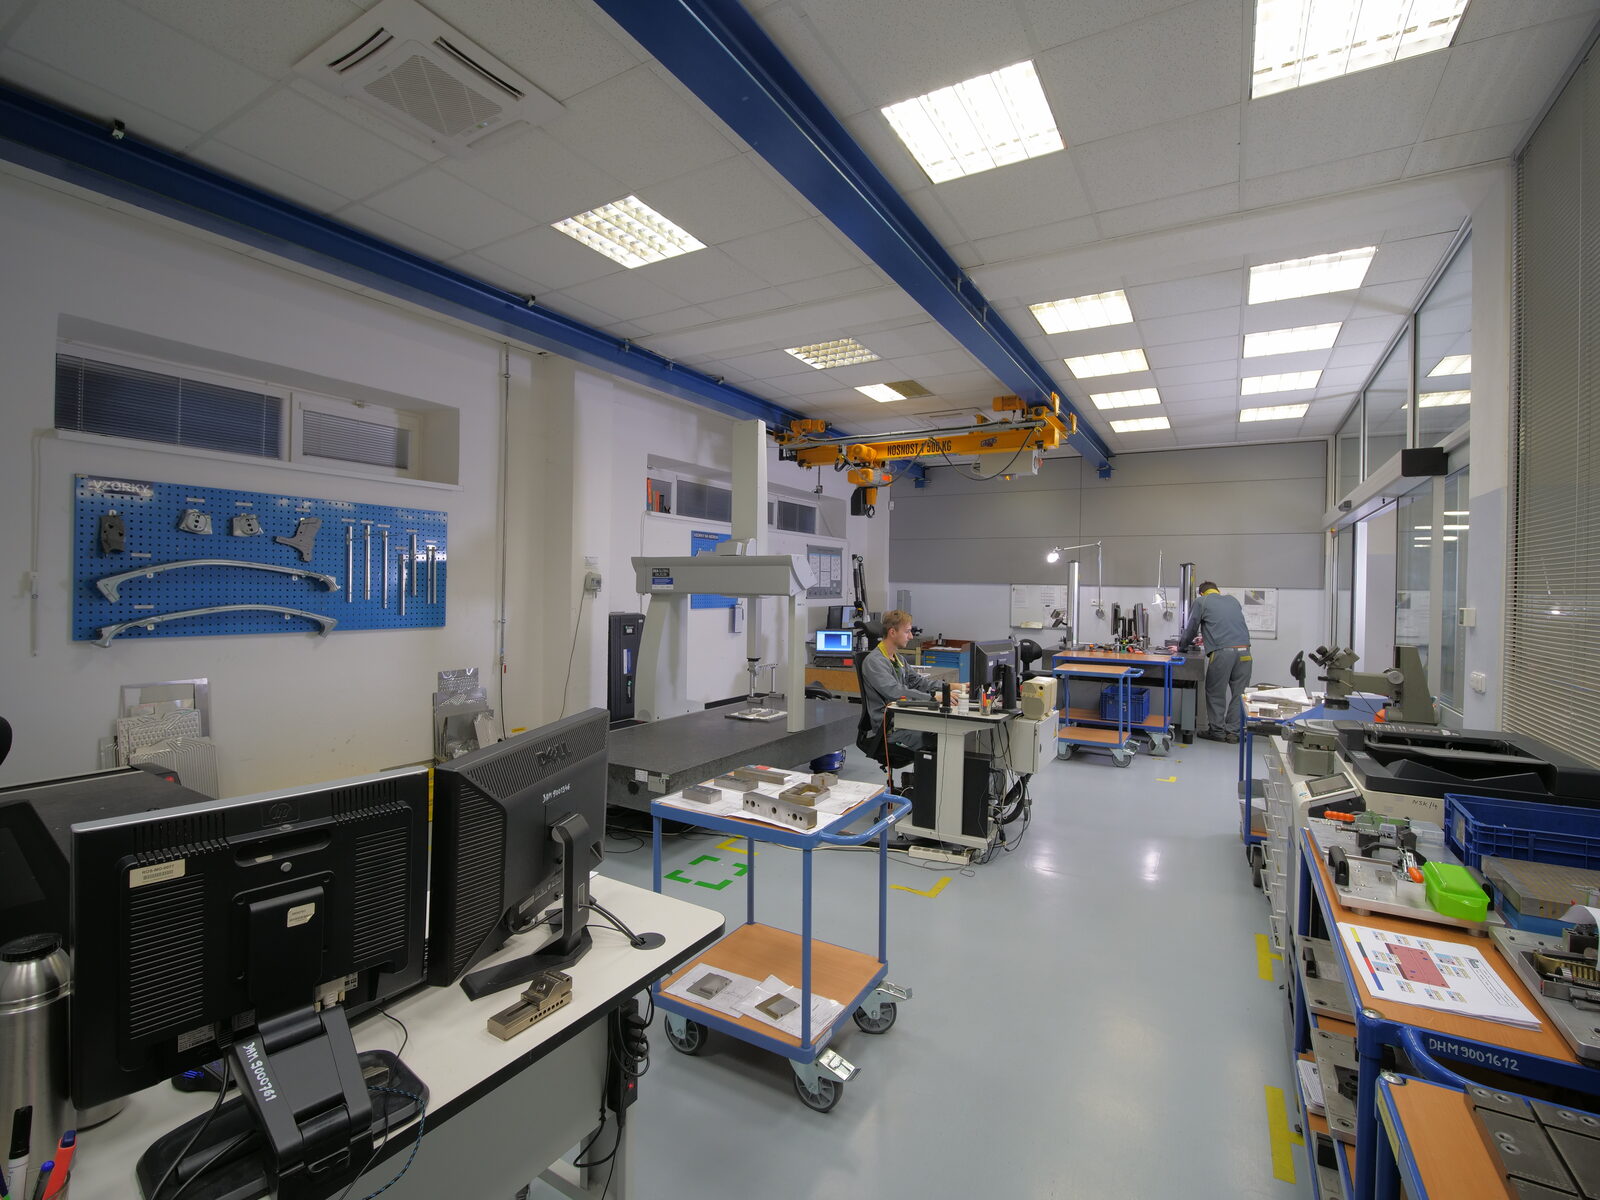
Every tool and every part is inspected before it is sent to the customer.
DEA Global
DEA Mistral
1996 / overhauled 2015Wenzel RS1215
Romer Absolute Arm 7525SI
Easyscope VID 3D MAN
3D microscope
Tesa Micro-Hite 600
1996–2011 (4 pcs)Dia Vite DH-5
Škoda PB 1
SWI-100
Also: magnetic particle inspection of safety parts and complete measurement documentation on the customer's request.
How a press tool is made: from design to the toolmaker's hands
A tool typically goes through six phases. Actual lead times depend on complexity — we give you an exact schedule after assessing your drawing.
3D design and simulation
Tool design in CAD, external stamping simulation, design approval by the customer.
Process planning
A production routing for every tool component — operation, machine, sequence.
Material purchasing
Tool steels, standard parts, guide elements.
CNC machining
Milling, wire EDM, die-sinking EDM. This is where the tool spends most of its time.
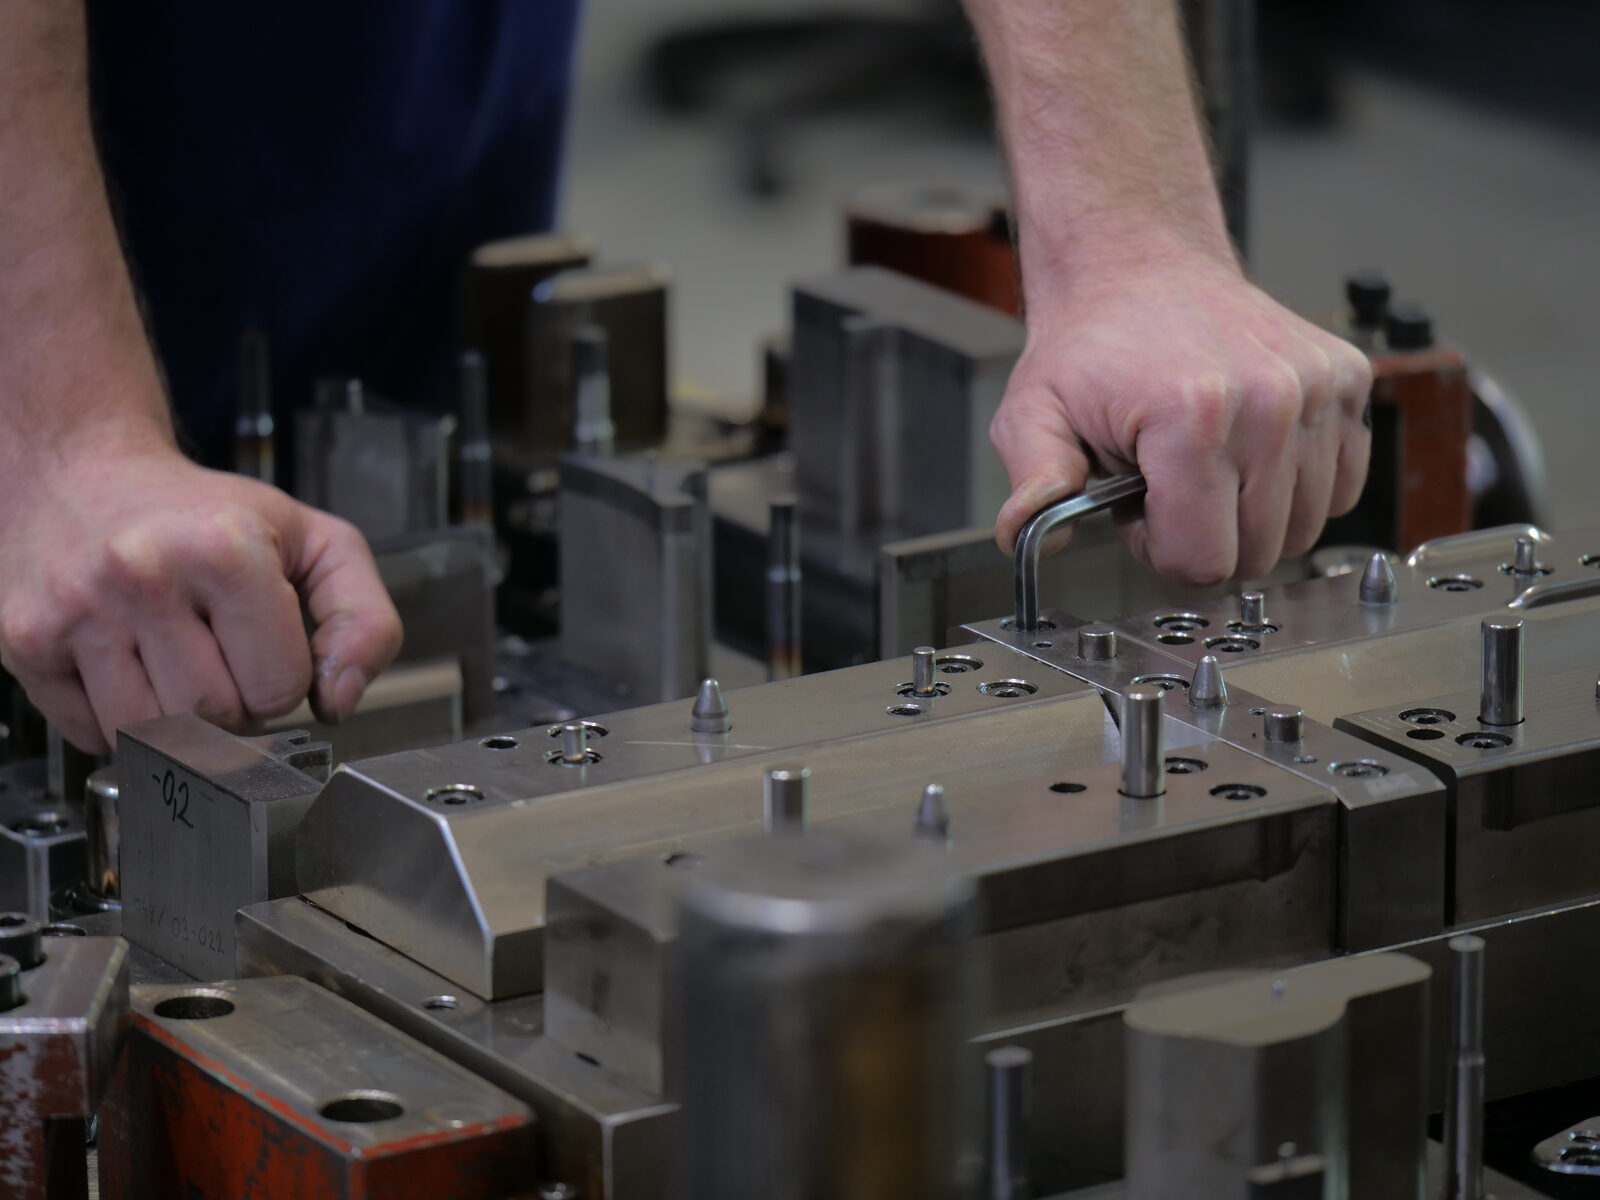
Assembly and try-out
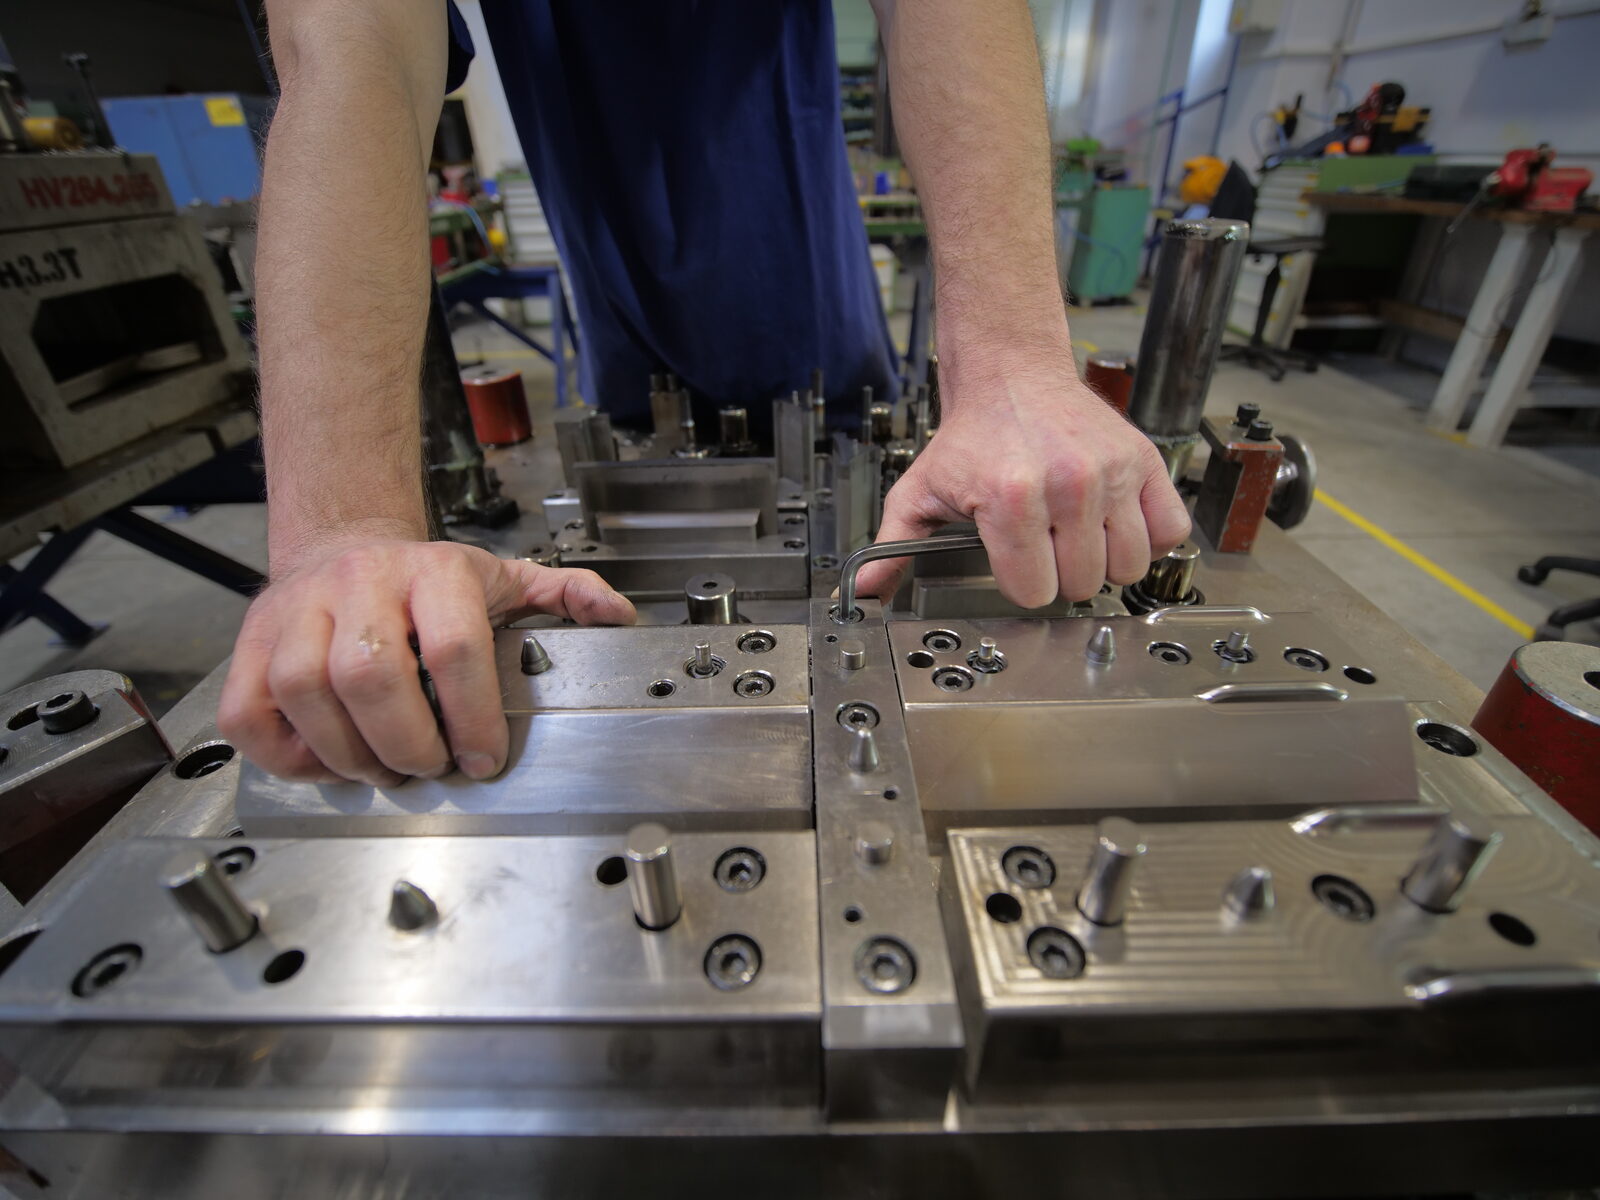
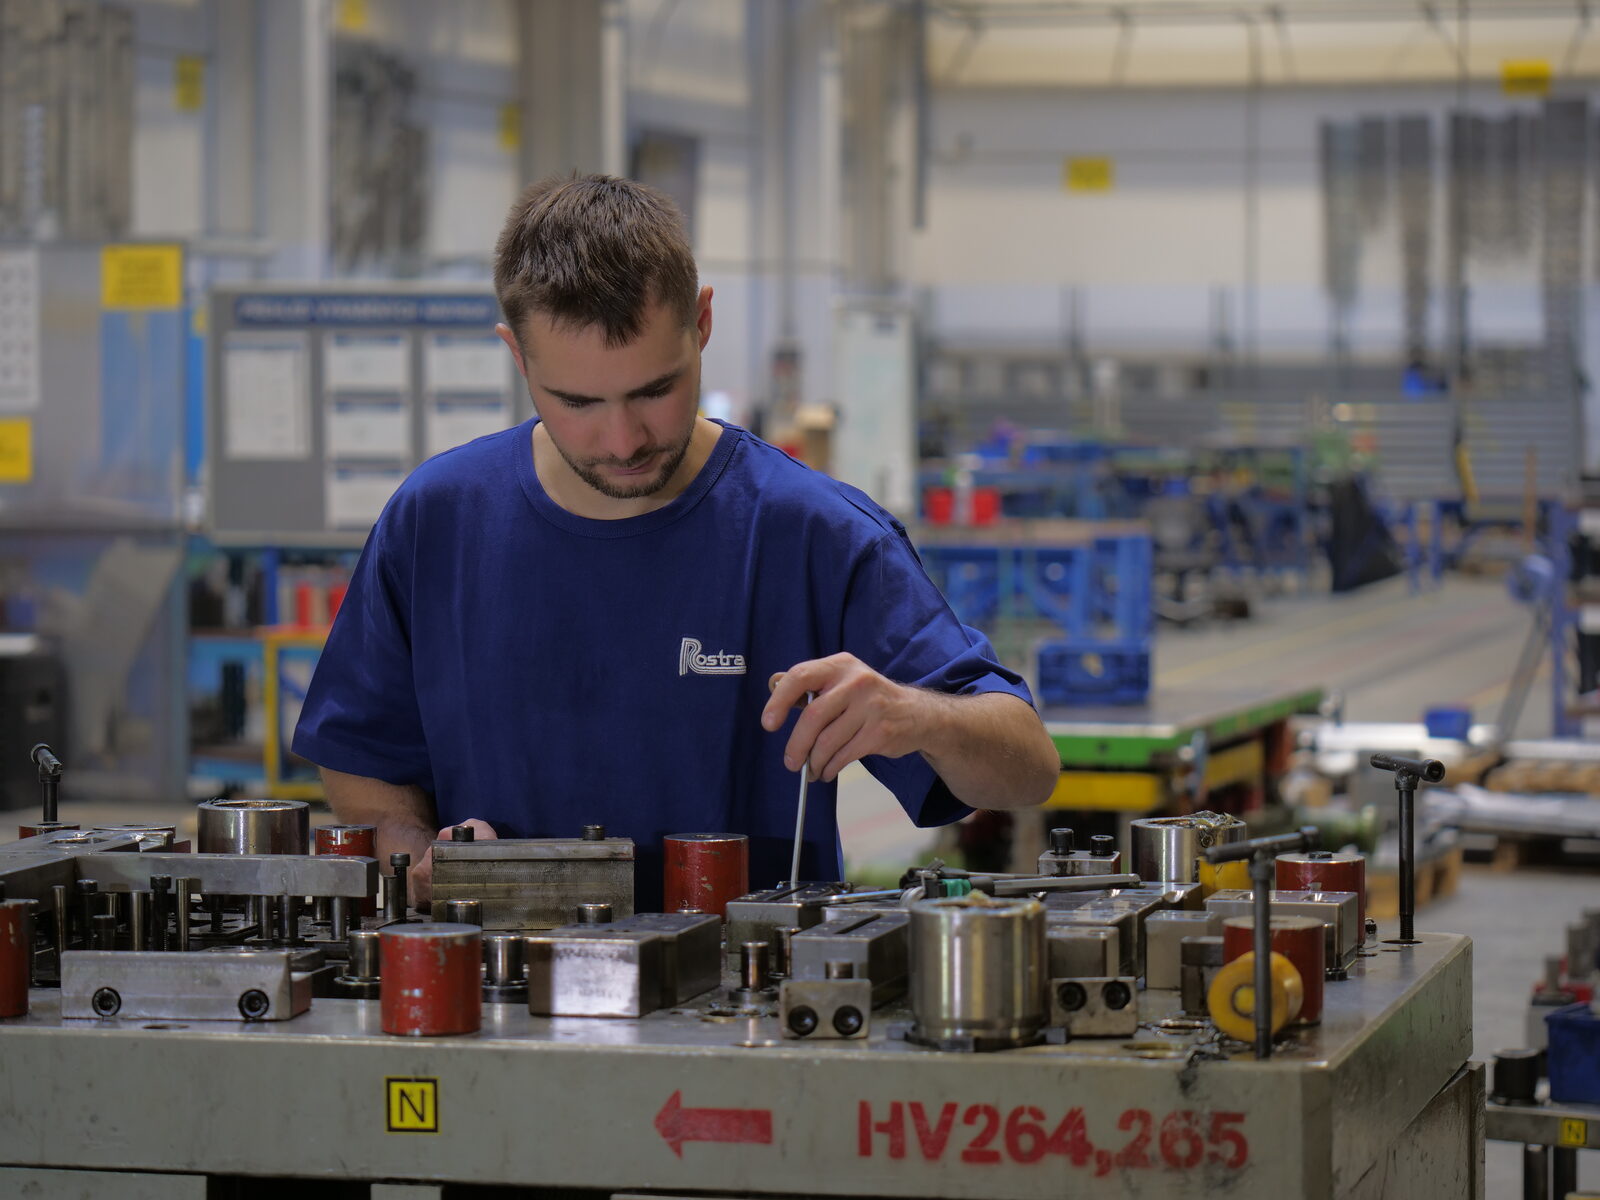
Assembling the tool, lapping, polishing, adjusting — the work of an experienced toolmaker.
Sample stampings and hand-over
Testing on a real press in our sister press shop, adjustments, hand-over with documentation.

Typical lead time [Typical lead-time range to be added]
Tool shop and press shop on one site
- Try-out on a real press. We try the tool out on a press of the right category, with no shuttling between companies.
- The tool can stay with us. Around 30 % of tools stay physically in the press shop — we stamp the parts from them ourselves.
- Lifetime maintenance. We handle repairs in-house — days, not weeks.
- Feedback into design. The designers see how the tool actually behaves in the press shop.
Outside automotive: racking systems for logistics centres
[Customer name to be added once they approve it] In recent years we have started making tools for racking systems used in large logistics centres. These tools require a specific approach to design — the parts are oversized and must withstand high loads over a long period.
The specifics of oversized, heavily loaded parts confirmed that automotive processes and precision transfer well to other industries. If you have a project outside automotive and are looking for a tool shop with automotive discipline, get in touch — we will assess feasibility free of charge.

Real projects from production
Our tools have produced parts for the projects BMW PL6/F07 (for Benteler), Daimler Staukasten (for Magna, Mercedes Actros), PSA T75 and projects for Audi, Seat and VW. Our injection moulds can be found on the parts VW BULB-CAP a VW FTI-HOLDER.
How it works
- Send us a drawing or part specification — via the form, or to rostra@rostra.cz.
- Sales registers the enquiry and passes it on for costing.
- The design department assesses feasibility — if the project is not a good fit for us, we tell you straight away.
- We send you a preliminary quotation including the recommended technology and an indicative lead time.
Response times vary with the complexity of the project [indicative number of working days to be added].
Sales contact
ROSTRA Tools tool shop
What types of press tools do you make?
Progressive, tandem and transfer press tools for automotive. We choose the tool type together with the customer according to material, batch size and the nature of the part. We also make injection moulds, forging dies, inspection fixtures and special assembly fixtures.
What is the largest tool you can handle?
Maximum tool length 5,000 mm, maximum weight 30 t.
Which CAD/CAM systems do you use?
Siemens NX, SolidWorks with SolidVision, and Visi for specialised tasks. We accept data in STEP and IGES as well as the native formats of these systems.
Do you do stamping simulations?
Yes. The simulations are done externally by specialists and the results are fed back into the tool design.
Can you also make an injection mould for plastics?
Yes, injection moulds are part of our standard production. References: VW BULB-CAP, VW FTI-HOLDER and others.
Can you try the tool out before hand-over?
Yes. Our own press shop, ROSTRA Stamping, with presses up to 800 t is on the same site — we try the tool out on a real press.
Can the tool stay in your press shop?
Yes. Around 30 % of tools remain the customer's property but stay physically in our press shop — we stamp the series parts.
Do you service and maintain the tool after delivery?
Yes, for the tool's whole service life. A standard repair typically takes days, not weeks.